

1. Safety: Pharmaceutical grade standards can be directly contacted
Compliance certification: Certified by FDA (US), EFSA (EU), YBB00102002 (China Pharmaceutical HDPE Bottle Standard)
2. Functionality: Naturally adapted to health products and food storage needs
High barrier properties: Outstanding moisture resistance, suitable for products that are easy to absorb moisture, such as fish oil, calcium tablets, protein powder, etc.
Light-shielding: Naturally opaque (transmittance <5%), no additional light-shielding coating is required, saving costs, and meeting the storage needs of photosensitive ingredients such as vitamins and probiotics.
Chemical resistance: Oil and fat resistance is better than PET.
3. Environmental protection: Significant carbon reduction, in line with ESG trends
Carbon footprint advantage: The production of RHDPE reduces carbon by 58%-60% compared to virgin HDPE.
Circular economy: The closed-loop recycling ratio is high, in line with the EU's mandatory requirement of 30% recycled packaging materials in 2025, and 100% local recycling is achieved.
4. Cost advantage: balance between performance and price
More economical than RPET: RHDPE does not require barrier coating for transparent bottles.
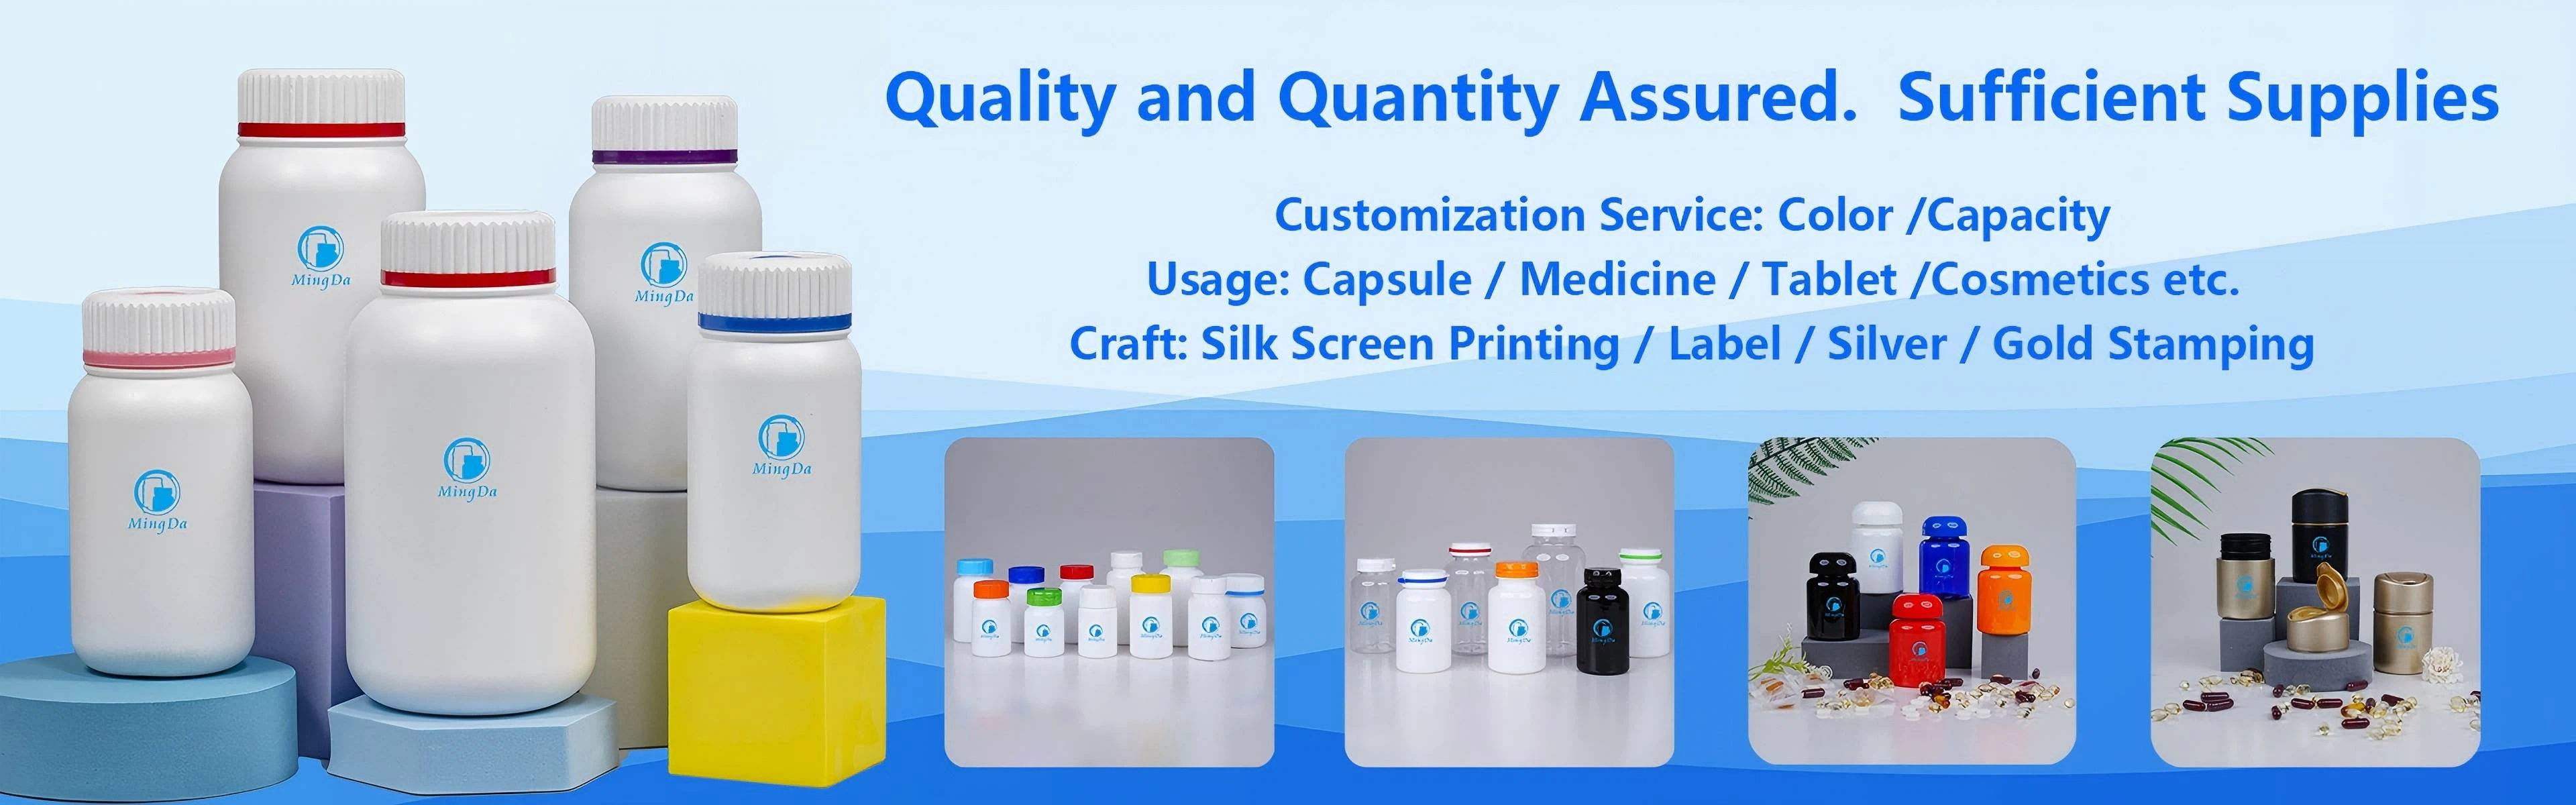
What are the application advantages of RHDPE materials in the health care food packaging industry?
Mar 17, 2025 Leave a message
Send Inquiry